

Reusable shopping bags can look correct at the sample stage but still develop problems during bulk production. Fabric shade can change between rolls, handles can shift during sewing, dimensions can move outside tolerance, and a print setup error can affect thousands of pieces before anyone notices it.
Reusable shopping bag quality control should therefore start with a defined product standard and continue through materials, production, testing, and final inspection. This guide explains what a good reusable shopping bag should achieve and the practical QC steps we use to keep bulk production aligned with the approved requirements.
What Makes a Reusable Shopping Bag Good Quality?
A good reusable shopping bag should use the right material, maintain structural integrity, consistently reproduce the approved dimensions and customisation, and perform as intended. Fabric, seams, handles, reinforcement, printing, dimensions, and accessories all influence the finished result. A lightweight non-woven promotional bag, a laminated woven PP grocery bag, and a heavy canvas tote have different materials, stress points, and performance expectations. We therefore judge each bag against its approved specification rather than applying one fixed standard to every design.

Fabric Quality and Material Consistency
The fabric should match the approved material specification and remain consistent across the production lot. Depending on the bag, that specification may include shopping bag material type, GSM, denier, weave, bonding structure, coating, lamination, colour, or recycled-content requirements.
Different materials need different quality priorities:
- Non-woven PP: GSM, bonding uniformity, surface condition, and colour consistency.
- Woven PP: weave consistency, lamination quality, surface flatness, and print substrate condition.
- Cotton and canvas: fabric weight, weave, natural shade variation, and dimensional stability.
- Polyester and RPET: fabric construction, denier where specified, coating, and roll-to-roll colour consistency.
Higher GSM does not automatically mean higher finished-bag quality. Fabric weight can affect body, strength, feel, and cost, but the material still needs to suit the construction and intended load. A heavier fabric cannot compensate for weak seams or poor handle attachment.
Consistency also matters in bulk production. Different rolls can meet the same nominal specification but still show visible differences in shade, texture, bonding, or lamination. These variations can become obvious when finished bags appear together in the same retail or promotional programme.
Strong Seams, Handles and Reinforcement
A good reusable shopping bag should maintain its structure under the intended load. The seams, handles, gussets, and bottom should work together to distribute weight without creating an obvious weak point. The bag should not show seam opening, excessive stretching, handle distortion, or loss of shape during normal use.
Depending on the bag type and expected load, the construction may use box stitching, cross stitching, additional stitch lines, extended webbing, or reinforcement patches at high-stress areas. A heavy canvas grocery bag usually needs more structural support than a lightweight promotional non-woven bag. The key is whether the finished construction provides enough support for the intended use, not simply how many reinforcement features it includes.
Accurate Dimensions and Consistent Customisation
Custom reusable bags also need to reproduce the approved size, shape, and branding within agreed tolerances. Important dimensions may include finished width and height, side or bottom gussets, handle length, handle drop, opening size, and the position of pockets or closures. Because sewn products naturally show some variation, the specification should define the critical dimensions, measurement method, and acceptable tolerance before production starts.
Branding needs the same control. We look at artwork version, logo size, orientation, print position, registration, colour, coverage, and overall appearance. For a bulk order, quality means more than producing one correct approval sample. It also means maintaining sample-to-bulk and bag-to-bag consistency across the production lot.
Performance Requirements for the Intended Use
The reusable shopping bag should perform under the conditions agreed for the project. Relevant requirements may include carrying capacity, seam integrity, handle strength, abrasion resistance, print durability, dimensional stability, or zipper and hardware function.
Those requirements change with the application. A lightweight promotional non-woven bag does not need the same structure as a woven PP grocery bag designed for repeated loading. A washable cotton tote may need colourfastness and shrinkage requirements that do not apply to a laminated shopping bag.
The intended application should set the performance target first. Testing then confirms whether the selected material and construction can meet that target. This is more useful than applying the same load, abrasion, or washing requirement to every reusable bag.
How Do We Control Quality in Reusable Shopping Bag Production?
Gentle Packing, as a reusable shopping bag manufacturer in China, controls quality from pre-production through final shipment. Approved specifications and samples set the production standard, while material inspection, in-process QC, and performance testing help identify problems before they affect the bulk order. Final inspection then verifies that the finished bags meet the agreed quality and packing requirements.
Specification and Pre-Production Sample Approval

The first QC step is to establish a clear production reference. Before we can decide whether a bag passes or fails, the production and QC teams need measurable requirements for the material, size, construction, branding, performance, and packing.
Before bulk production, we normally confirm the following:
- Material specification: Fabric type, GSM, denier, weave, coating, lamination, or other relevant material requirements.
- Finished dimensions: Width, height, gussets, handle dimensions, and other critical measurements.
- Tolerance: Acceptable production variation for the dimensions or positions that matter to the project.
- Construction: Seam type, handle attachment, reinforcement, closures, pockets, and other structural details.
- Customisation: Approved artwork, print method, logo dimensions, print position, and colour reference.
- Performance requirements: Intended carrying load or other required functional tests.
- Packing requirements: Unit packing, carton quantity, labels, barcodes, and carton marks.
We also review critical-to-quality points before bulk production. A grocery tote may place more importance on handle attachment and bottom construction, while a promotional bag with a large multicolour design may require tighter print-position and registration control.
The pre-production sample then confirms whether those requirements work together as a finished product. It allows us and you to evaluate proportions, construction, printing, hand feel, and assembly before we release bulk production. But note that the sample does not replace the specification. An inspector cannot determine an exact GSM, dimensional tolerance, artwork version, or required carrying load simply by looking at a physical sample. We therefore use the specification, artwork, and approved sample together.
Incoming Fabric and Component Inspection
Incoming inspection checks whether the fabric, components, and supporting material records match the approved reusable bag specification before production starts. The focus is on material accuracy, batch consistency, and any compliance requirements defined for the order.
| QC Area | What We Check | Our Control Method |
| Fabric | Material construction, GSM, width, shade, weave/bonding, coating or lamination | Measure against the specification, verify GSM by sample weighing, inspect surface condition, and compare fabric rolls |
| Components | Handles, webbing, cords, zippers, hardware, labels, reinforcement pieces | Check dimensions, colour, construction, and function against the approved sample and specification |
| Material lots | Shade, GSM, surface finish, lamination, component consistency | Compare rolls or batches before mixing them into the same production run |
| Compliance | Certified material claims and required chemical documentation | Check applicable certificates, traceability records, and test reports against the actual material used |
For fabric, GSM should be verified by weighing a sample of known area rather than relying on hand feel. On larger orders, we also compare different rolls before cutting. Two rolls may meet the nominal specification but still show visible differences in shade, weave, bonding, or lamination. Material outside the approved range should be separated before it reaches production.
Compliance checks depend on the project. For certified RPET bags, for example, we verify that the certification and traceability documents correspond to the supplier and material used for the order. Where chemical testing is required, the report should match the relevant material and colour rather than refer only to a similar product. This keeps certification and compliance tied to the actual reusable bag order, not just to a general supplier claim.
In-Process Inspection During Cutting, Printing and Sewing
In-process inspection is used to catch a repeatable production deviation before it affects a large part of the order. The first completed production pieces are compared with the approved sample before full-volume production continues. After approval, periodic checks help identify process drift during longer production runs.
| Production Stage | What We Check | Our QC Action |
| Cutting | Panel size, gusset, sewing allowance, alignment | Measure first pieces and periodic production pieces |
| Printing | Artwork, logo position, colour, registration, coverage | Approve first printed pieces before continuing |
| Sewing | Seam construction, handles, reinforcement, gussets, bottom | Check first completed bags and repeat during production |
Cutting Accuracy and Panel Consistency

Cutting directly affects the finished size, symmetry, gusset shape, and print position of a reusable shopping bag. Once a panel is cut too small or off-position, sewing usually cannot fully correct the error. Before bulk cutting, we compare the cutting pattern and first cut pieces with the approved bag specification to confirm the required size and seam allowance.
Our main QC focus includes:
- Panel dimensions
- Gusset dimensions
- Sewing allowance
- Cutting orientation
- Stack consistency
- Cut-edge condition
During bulk cutting, our QC team checks dimensional consistency across the cutting stack and repeats measurements when the fabric roll, stack height, blade, or cutting setup changes. Fabric movement, stack compression, or blade wear can cause size variation, uneven gussets, insufficient seam allowance, or rough edges. When we find a systematic deviation, we separate the affected pieces, adjust the cutting setup, and check a new set of panels before sending them to sewing.
Printing Control Against Approved Artwork

Printing QC starts with the approved artwork and colour reference. Before the full print run continues, the first acceptable printed pieces are checked for logo size, position, orientation, colour, registration, and overall coverage.
The control method also depends on the printing process. For example:
- Screen printing requires attention to registration, ink coverage, edge definition, and curing.
- Heat transfer requires accurate positioning, stable adhesion, and clean edges.
- Sublimation requires colour consistency and image clarity.
- Printed laminated woven PP needs both print consistency and stable lamination appearance.
Sewing, Handle Attachment and Structural Control

Sewing QC checks whether the reusable shopping bag keeps the approved structure and load-bearing strength during production. We focus on seam allowance, stitch consistency, handle position, handle attachment, reinforcement, gussets, and bottom seams. Handle and bottom areas receive extra attention because they carry most of the load during use.
We set the stitching and reinforcement method according to the bag material, construction, and intended load. Canvas, polyester, non-woven PP, and woven PP do not use the same sewing settings. Where needed, we use box stitching, cross stitching, additional stitch lines, or reinforcement patches to reduce stress around handles and other high-load areas.
Functional and Durability Testing
Functional and durability testing shows whether the finished reusable shopping bag can handle the conditions it was designed for. The test plan changes with the material, bag structure, expected load, printing method, and accessories, so each project focuses on the most relevant failure risks rather than following one fixed test routine.
| Test | Main Purpose | Key Check Points |
| Load test | Verify carrying performance | Handles, attachment points, seams, bottom, deformation |
| Drop test | Check resistance to impact | Bottom, corners, seams, handle attachment |
| Abrasion test | Evaluate surface wear | Fabric surface, coating, print area |
| Print/colour durability | Check branding durability | Rubbing, transfer, adhesion, fading |
| Zipper/hardware test | Verify functional components | Operation, attachment, wear |
Load Test
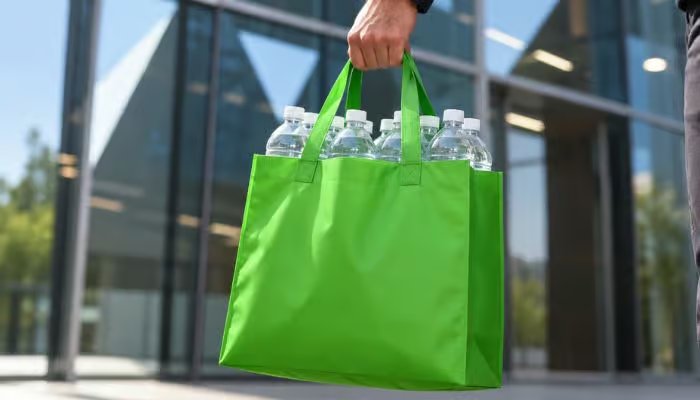
For a bag with a defined carrying requirement, we test the finished structure under that load. For example, if the target is 10 kg, we can place about 10 kg of bottled water inside the bag to create a practical, evenly distributed load, then lift or suspend it for the agreed time or number of cycles.
After testing, we inspect the handle attachment, side and bottom seams, gussets, and bag body for opening, tearing, excessive stretching, or permanent deformation. If the project also requires controlled seam-strength testing, ISO 13935-1:2014 uses a strip method to measure the maximum force needed to rupture a sewn seam. ISO mainly applies this method to woven textile fabrics, so nonwoven PP, coated fabrics, and polyolefin tape-yarn constructions may require a different test approach.
Drop Test
A drop test checks how the bag responds to sudden impact rather than a steady load. We fill the bag to the agreed weight, drop it from the specified height and direction, and repeat the test where the project requires multiple drops.
The main inspection points are the bottom seam, corners, gussets, handle attachment, and bag body. This test is more relevant for grocery bags or other designs that may carry heavier contents and experience accidental drops during normal use.
Abrasion Test

Abrasion testing checks how the surface of finished reusable bags holds up under repeated rubbing. It is especially relevant for canvas bags, cotton tote bags, polyester shopping bags, and other reusable bags that regularly contact clothing, counters, floors, or other rough surfaces during use.
We look for surface wear, fibre damage, coating deterioration, colour change, and print wear. For applicable textile fabrics, ISO 12947-2:2016 specifies the Martindale method for determining abrasion breakdown. The standard applies to textile fabrics including nonwovens, but excludes coated and laminated fabrics, so laminated woven PP shopping bags may require a different test approach.
Print and Colour Durability Test
Printed reusable bags need durability tests that match the printing method and expected use. Depending on the project, we may test rubbing resistance, adhesion, colour transfer, cracking, peeling, or washing performance. A washable cotton tote may need rubbing and laundering checks, while a heat-transfer logo needs closer attention to adhesion and edge lifting.
For dyed or printed textile surfaces, ISO 105-X12:2016 provides a standard method for evaluating colour transfer caused by rubbing. The QC focus also changes with the printing process: screen printing may need checks for ink loss or cracking, while laminated woven PP bags may require both print durability and lamination-bond checks.
Zipper and Hardware Test

For bags with zippers, snaps, buckles, eyelets, or other functional hardware, we check both operation and attachment. A zipper may be opened and closed repeatedly to confirm smooth movement, proper alignment, and secure attachment to the bag.
After testing, we inspect the zipper tape, stitching, puller, surrounding fabric, and hardware for loosening, deformation, or damage. Where repeated use is important, the project can define a specific cycle requirement before production.
Final Inspection and AQL Sampling

Final inspection confirms that the finished reusable shopping bag lot still matches the approved requirements before shipment. Our QC team selects samples from the actual production lot and compares them with the approved sample, artwork, and tolerance standards. We check finished dimensions, construction, printing, workmanship, accessories, function, quantity, and packing. For multi-colour or multi-SKU orders, we spread the samples across different variants instead of checking only one group.
For larger orders, we can use AQL sampling to evaluate whether the lot meets the agreed acceptance level. The lot size, inspection level, selected AQL, and defect classification determine the sampling plan. We normally classify defects as critical, major, or minor according to their effect on safety, function, specification, branding, or appearance. A broken handle, open structural seam, wrong artwork, or major size deviation may count as major, while a small cosmetic issue may count as minor. Both sides should agree on the defect criteria before inspection so the QC team can apply the same standard throughout the evaluation.
If the sample exceeds the agreed limit, we isolate the affected lot, identify the cause, sort or rework the products where necessary, and inspect the corrected lot again. Before shipment, we also verify carton quantity, SKU separation, labels, barcodes, carton marks, and shipping marks. We release the order only after both the reusable bags and the packing configuration meet the approved requirements.
Conclusion
Consistent reusable shopping bag quality comes from controlling the right points at the right stage. Clear specifications set the standard, incoming inspection keeps unsuitable materials out of production, in-process checks prevent repeatable defects, and performance testing confirms whether the finished bag can handle its intended use. Final AQL sampling then gives both buyer and manufacturer a clear basis for shipment approval.
Reusable bag projects often involve specific requirements for load capacity, size tolerance, colour matching, recycled materials, or retailer inspection standards. Gentle Packing can review these requirements during sampling and carry the agreed QC points through bulk production, testing, and final inspection.
